Pneumatic Action Chain for Carton Erecting Machines
A station-level guide to carton pickup, vacuum proof, panel opening, flap folding, format changeover, and controlled recovery from missed or doubled blanks.
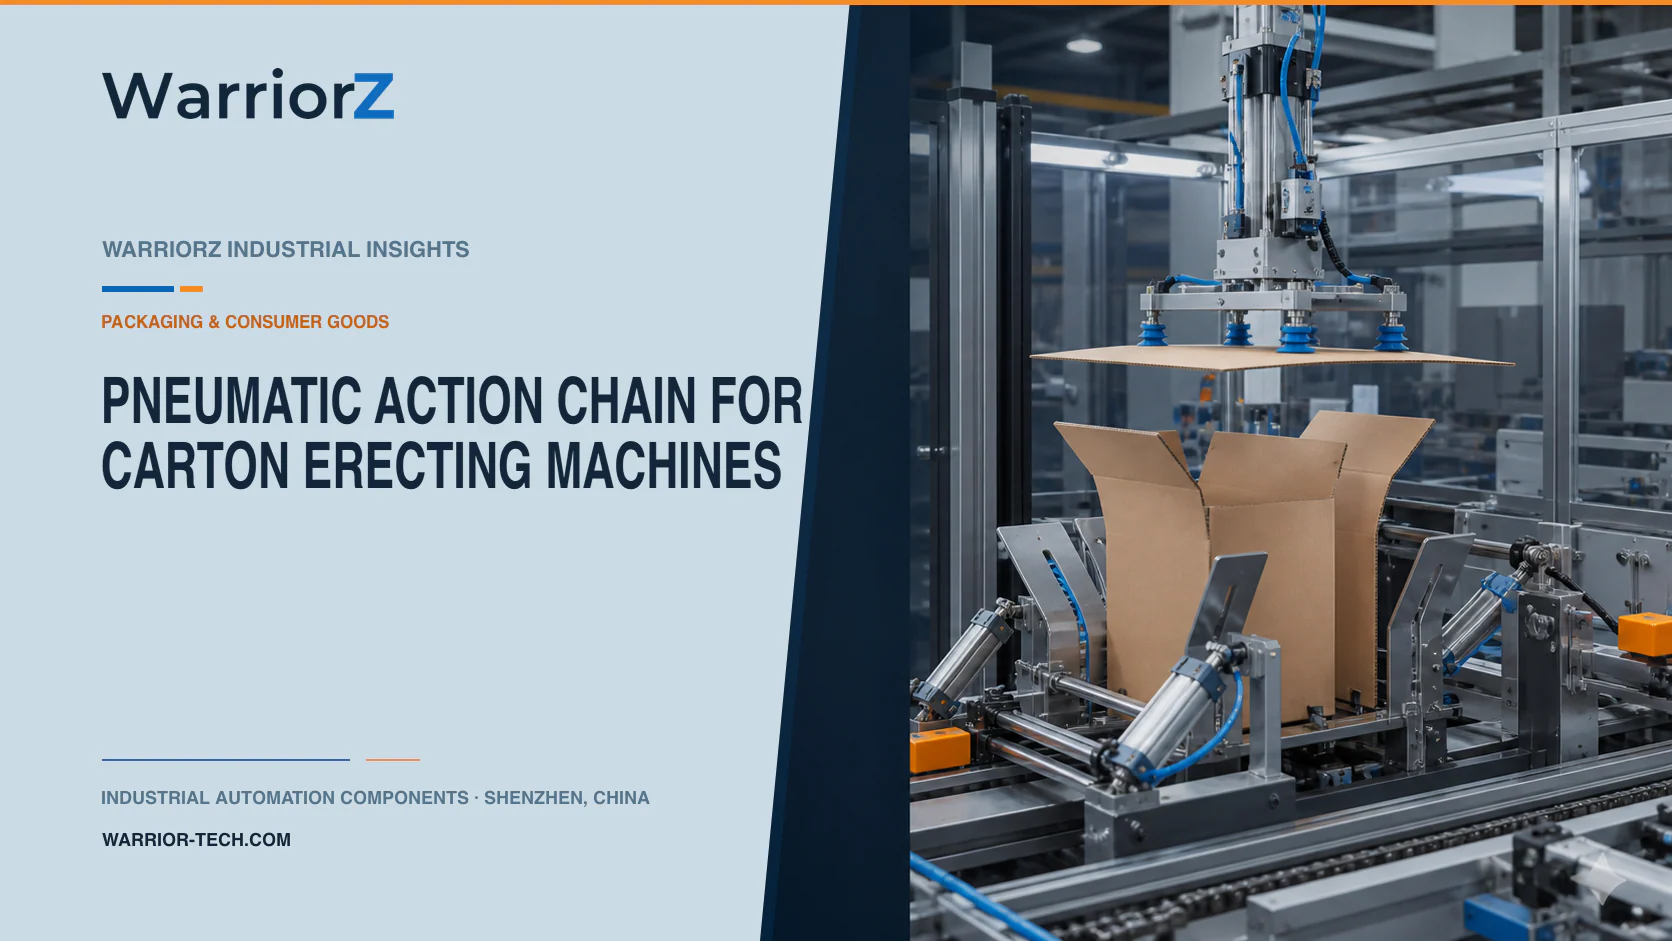
A carton erector turns a flat corrugated blank into an open case ready for filling. Vacuum cups separate one blank from a magazine, an opening mechanism pulls opposing panels apart, cylinders fold the bottom flaps, and a closing or sealing station holds the geometry. Reliable operation depends on proving each material state before the next action, not on running a fixed set of timers.
WarriorZ provides application-oriented product information and component sourcing support for pneumatic systems. The equipment OEM owns the mechanism, pneumatic circuit, controls, safeguards, and conformity work. The factory owns approved carton specifications, operating limits, inspection criteria, maintenance, and safe work procedures.
Map the blank path before choosing hardware
Record magazine orientation, blank dimensions, flute and board grade, coatings, print surfaces, score locations, manufacturer's joint, flap style, warp allowance, and line rate. Identify every contact surface. A cup that works on an unprinted liner may leak on a porous, dusty, or deeply embossed panel.
The sequence should describe physical states. Blank available, single blank acquired, blank clear of magazine, case opened, opposed panels separated, minor flaps folded, major flaps folded, and case transferred are more useful than cylinder numbers. Each state needs a sensor or validated inference appropriate to the consequence of failure.
Process state | Actuator task | Confirmation | Stop condition |
|---|---|---|---|
Blank presented | Magazine controls expose one sheet | Blank present and stack not empty | No blank or double-feed risk |
Vacuum pickup | Cups seal and lift | Vacuum threshold reached in time | Leak or failed acquisition |
Extraction | Axis clears guides | Position and vacuum remain valid | Blank catches or drops |
Case opening | Puller separates panels | Opening geometry detected | Joint stuck or blank folded wrong |
Bottom folding | Cylinders fold in sequence | Case held and flap path clear | Flap collision or missing case |
Transfer | Conveyor accepts erected case | Receiving zone available | Downstream backup |
Size the vacuum path for real corrugated board
Cup selection depends on available contact area, surface texture, leakage, acceleration, cup orientation, blank mass, and the effect of a pressure mark. Test samples from approved suppliers, including warped and low-friction conditions. Place cups away from scores, slots, loose labels, and critical print when the surface requirement demands it.
Festo's official VAS and VASB suction cup data documents different cup shapes, sizes, and materials and points users to a vacuum engineering tool. The OVEM vacuum generator data lists vacuum generation, sensing, ejector pulse, filter, and interface options. Use these documents as product-specific selection inputs. They do not qualify a cup and generator combination for a particular carton.
Keep vacuum tubing short and protected when response time matters. Include fittings, manifold volume, filters, cups, and deliberate leakage in testing. A generator's catalog vacuum value does not describe the pressure reached at a leaking cup on corrugated board.
Detect empty picks and double blanks
Set a pickup decision window from measured vacuum curves for valid blanks, empty cups, badly leaking blanks, and doubled sheets. A threshold by itself may not distinguish all cases. Add thickness, displacement, optical, or mechanical checks where a double blank could jam the opening station.
Fault | Expected signal pattern | Machine response | Inspection target |
|---|---|---|---|
Empty pick | Vacuum fails to build | Return safely and retry by defined limit | Cup, magazine, and blank presence |
Leaking blank | Slow or unstable vacuum | Reject or stop before extraction | Porosity, warp, score under cup |
Double blank | Vacuum may appear normal | Use independent sheet check | Magazine separation and static |
Dropped blank | Vacuum falls during travel | Stop before fold mechanisms move | Hose, cup wear, acceleration |
Stuck manufacturer's joint | Vacuum remains but case stays flat | Release without forcing fold | Adhesion and blank specification |
Avoid endless automatic retries. Repeated pickup attempts can empty compressed air into the area, damage the top blank, or create an unexpected stack condition. Define a retry limit and a recovery position where the operator can see the fault without entering a hazardous zone.
Open the case without tearing scores
Support one panel while the vacuum puller moves the opposing panel. The motion should follow the intended score lines and avoid twisting the manufacturer's joint. Tune cylinder speed under the full blank range. A high initial breakaway acceleration can peel a cup or buckle a weak panel even if the end position looks correct.
Use mechanical guidance to establish the open case geometry. Pneumatic cylinders should move the opening mechanism, not act as the only alignment reference. Provide adjustment references for format changeover and lock them against drift. When a mechanism can overtravel, fit a designed stop or guided axis instead of using the carton as the stop.
Confirm that the case is open before folding flaps. A sensor looking at cylinder position proves the mechanism moved, while a separate case geometry check can detect a blank that slipped or never opened.
Fold flaps as a controlled action chain
Minor and major flap folders need clearance and order. Model the paths at the smallest and largest cases, with warped flaps and realistic conveyor variation. One flap can rebound into the next cylinder's path after its actuator retracts.
Use flow control, cushioning, and actuator sizing to produce the needed movement without striking the board. Do not hide a poor folder profile by increasing air pressure. When format changes alter lever arms or contact locations, revalidate the force and stroke.
Festo's industrial packaging page gives a first-party overview of automation approaches for industrial packaging. It is context, not a finished carton-erector design. The OEM still needs a machine-specific calculation and test record.
Design changeover as part of the machine
List every format point: magazine width, blank stop, cup position, puller stroke, opening guide, flap tools, conveyor guides, and sensor windows. Use scales, keyed locations, recipes, or verified automatic axes. A saved pneumatic timing recipe cannot correct a guide left at the wrong position.
Teach vacuum thresholds with controlled samples and protect the approved values. Inspect cups for hardening, cuts, contamination, and deformation. Check filters and silencers using condition and documented intervals. A slow vacuum curve can indicate board leakage, a worn cup, restricted flow, or a tubing fault, so diagnostics should preserve the trace rather than naming one cause.
Guard the magazine, puller, and flap tools
The magazine, moving pickup head, opening linkage, flap folders, and conveyor create pinch, crush, and drawing-in hazards. ISO 12100:2010 provides a general risk-assessment framework. ISO 4414:2010 addresses pneumatic system hazards and relevant life-cycle activities.
Define the response to air loss, power loss, vacuum loss, a jam, and an opened guard. A retained blank may fall when vacuum vents. A cylinder may move when trapped pressure is released. Select safe states and protective measures from the machine risk assessment.
Process vacuum switches and end sensors do not automatically serve a safety function. The OEM must specify safeguards, reset logic, diagnostic coverage, and validation separately. The factory must isolate hazardous energy before clearing a trapped carton, replacing cups, or reaching into the folding section.
Commission with carton variation and faults
Run each approved case at relevant board grades, flute directions, coatings, print areas, warp limits, stack heights, humidity conditions, and line speeds. Record pickup curves, extraction position, opening confirmation, fold results, case squareness, damage, and reject causes.
Challenge an empty magazine, missed pick, double blank, porous panel, warped blank, blocked vacuum line, worn cup, low supply, stuck joint, lost vacuum in motion, wrong format, flap rebound, downstream backup, and interrupted cycle. Recovery must discard or re-establish any case whose state cannot be proven.
For the next operation in a packaging cell, see pneumatic pusher design for horizontal cartoners. To review vacuum, cylinders, valves, and sensing from real carton samples, send a WarriorZ carton-erector inquiry.
Official sources
Sources and verification basis
These references support the documented facts, calculations, or engineering boundaries used in this article.