Pneumatic Side-Push Carton Packing: Controlling Bottle-Tipping Risk
A beverage-line guide to guided pusher design, stroke-by-stroke speed control, carton and group interlocks, fallen-bottle detection, and broken-glass recovery.
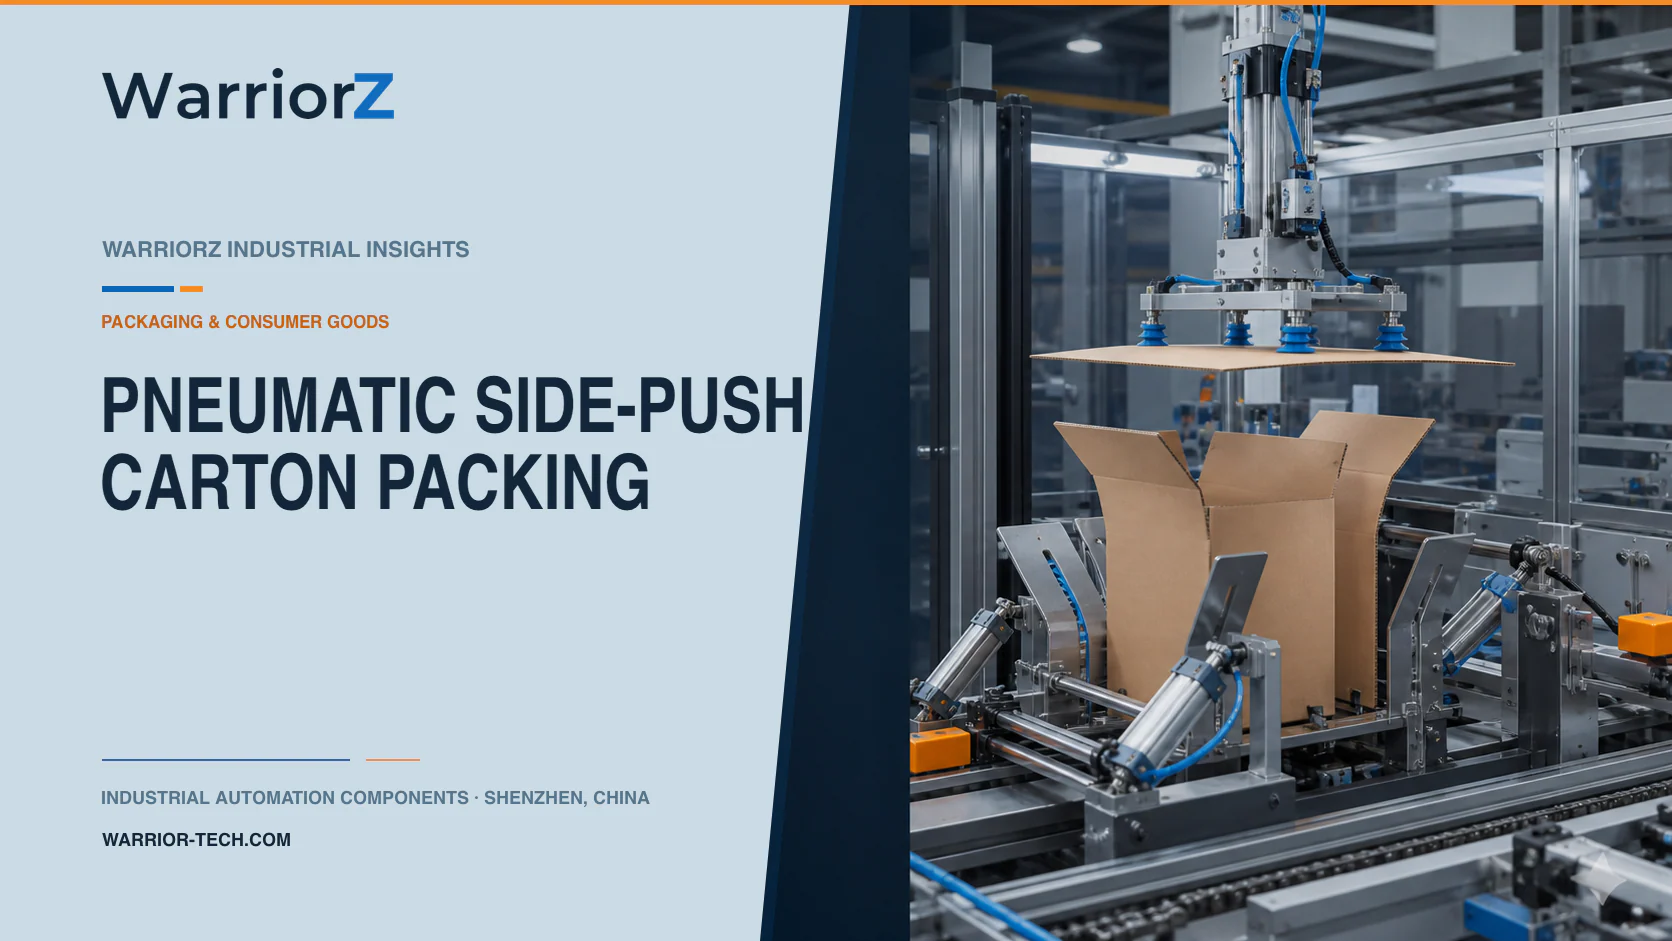
A beverage cartoning cell meters bottles or cans on a conveyor, stops them in a defined matrix, aligns the group with an open carton, and pushes the group sideways into the case. The pneumatic pusher must overcome guide and carton-entry resistance without tipping containers, striking glass, scuffing labels, or compressing a weak pack.
WarriorZ helps factories and equipment builders identify and source pneumatic components from model numbers, photographs, drawings, and BOMs. The OEM owns the mechanism, actuator and valve sizing, controls, safeguards, and line integration. The factory owns container and carton specifications, product-loss controls, hygiene, broken-glass procedures, maintenance, and acceptance testing.
Characterize the container group and carton entry
Record container material, diameter, height, mass, fill level, center of gravity, base geometry, surface friction, label type, cap or closure, group pattern, and allowable contact. Include wet bottles, condensation, label adhesive, line lubricant, and temperature when they occur in production.
Measure the carton opening, flap position, internal dividers, board stiffness, and guide transition. A group that is stable on a flat conveyor can tip when the first row crosses a gap or meets a divider. The pusher plate, dead plate, carton guide, and receiving support must act as one mechanical path.
Input | Effect on side push | Trial requirement |
|---|---|---|
Container center of gravity | Sets tipping sensitivity | Tallest and least stable approved format |
Base and conveyor friction | Changes breakaway and row compression | Dry and approved wet conditions |
Glass strength and defects | Limits impact tolerance | Factory quality and handling rules |
Carton opening | Creates entry resistance and snag points | Worst qualified warp and flap position |
Group pattern | Changes load sharing across rows | Every approved count and divider style |
Transfer gap | Can catch the leading row | Measured alignment under line load |
Guide the pusher and spread contact
Use a wide plate that contacts the approved region of the last container row or a product-specific carrier. Keep the plate perpendicular to travel. A guided axis should carry side loads and moments created by the wide plate, while the cylinder supplies thrust.
Festo's official DFM guided drive data lists product-specific guide, load, cushioning, sensing, and environmental information. It can support an engineering comparison, but it does not qualify a DFM for a wet beverage line or glass handling. The OEM must calculate the real plate mass, offset, guide loads, cycle rate, washdown exposure, and stopping forces.
Provide a mechanical reference for home and insertion. The carton, bottles, or internal divider must not serve as the actuator stop. If multiple formats use different insertion positions, use qualified stops or position control and prove the selected setting before automatic operation.
Shape speed across the complete stroke
A slow average speed can still include a sharp breakaway and a hard entry impact. Measure velocity through release from the grouping stop, approach to the carton, entry, and final placement. Adjust flow controls and cushioning under loaded conditions. Supply pressure, seal friction, payload, back pressure, and restricted exhaust can change the profile.
Use the lowest thrust and acceleration that complete the qualified move. Increasing pressure to clear a recurring resistance can increase bottle contact loads and hide a misaligned guide. If the mechanism needs a fast return for cycle time, separate return settings from the loaded forward stroke.
Stroke zone | Desired behavior | Evidence | Fault limit |
|---|---|---|---|
Initial breakaway | Start without compressing the rear row | Motion trace and product observation | Sudden row impact |
Group acceleration | Keep all containers supported | No relative row movement | Tipping or label scuff |
Carton approach | Align before entry | Guide and carton position valid | Closed flap or skewed carton |
Entry | Maintain controlled force and speed | Stable leading row | Rising resistance or fallen bottle |
Final placement | Reach qualified insertion depth | Position and pack geometry | Overtravel into carton wall |
Retraction | Clear before carton transfer | Home state proven | Plate catches trailing product |
Interlock grouping, carton presence, and push permission
Do not command the pusher until the correct count and group geometry are established, the grouping stop is in the qualified state, the carton is present and open, the receiving path is clear, and downstream transfer is ready. One photoelectric count can miss a fallen or nested container, so use sensing and guides appropriate to the failure risk.
Monitor forward travel. A position timeout detects slow motion, while a characterized pressure or force signature can help identify resistance. Neither should force continued movement. On disagreement, stop additional product feed and place the pusher in the risk-assessed state.
Keep the carton clamped or guided until the group reaches the approved position. Release the carton only after the pusher clears the transfer path. If an interrupted cycle leaves some containers in the carton and some on the dead plate, require a controlled recovery rather than restarting from a count signal.
Prevent and detect fallen containers
Use rail height, lateral clearance, dead-plate support, and plate profile to keep the group upright. Avoid gaps that accept a bottle heel or can rim. Verify the path with the least stable container, the lowest fill mass, and approved wet conditions.
Place fallen-container detection where it can see a container before the pusher traps it. A pressure spike after contact arrives late. If transparent containers or reflective cans challenge optical sensing, test the actual finishes and backgrounds. Preserve the failed image or sensor trace when practical for troubleshooting.
For glass, define containment and cleanup before commissioning. Broken fragments can enter guides, cylinder seals, conveyors, cartons, and nearby open product. The factory's glass-control and hygiene program must decide the affected area, product hold, cleaning, inspection, and release. Pneumatic blow-off should not scatter fragments through the cell.
Design for the beverage environment
Select component materials, protection, tubing, fittings, lubricants, and mounting from measured moisture, cleaning chemical, temperature, and contamination conditions. Keep exhaust away from open containers and product contact zones. A stated enclosure rating for one component does not qualify the complete assembly after connectors and custom wiring are installed.
Provide inspection access for the pusher pad, guide, stops, dead plate, and carton guides. Product residue can change friction and make a previously stable recipe tip containers. Tie cleaning verification to startup checks after sanitation or a spill.
Guard crush points and control stored energy
The side pusher, grouping stops, carton clamp, conveyors, and guides create crush, shear, and trapping hazards. OSHA's machine guarding general requirements describe protection around points of operation and moving parts. ISO 12100:2010 provides general machinery risk-assessment principles, while ISO 4414:2010 covers pneumatic-system hazards.
Define the safe response to air loss, power loss, guard opening, carton jam, fallen bottle, and broken glass. Venting can allow a loaded pusher or stop to move. Trapped pressure can release when a jammed group shifts. The OEM must design safety functions and validation separately from process sensing.
The factory must isolate and verify hazardous energy before reaching into the push path, removing glass, or adjusting guides. Where gravity, springs, or retained products can move after isolation, provide the required restraint and procedure.
Qualify formats and fault recovery
Run every approved container, fill level, group pattern, carton, divider, label, cap, conveyor condition, speed, and supply extreme. Inspect tipping, glass contact, label scuff, can denting, group geometry, carton damage, insertion depth, and downstream closure.
Challenge a missing bottle, extra bottle, fallen bottle, skewed group, missing carton, partial carton opening, wrong divider, wet dead plate, low supply, blocked exhaust, sensor offset, loose guide, pusher jam, carton backup, and interrupted stroke. Recovery must establish the actual count and location before automatic feeding resumes.
For the case-closing step after packing, see adaptive pneumatic beams for random case sealers. For a component review based on container and carton trials, send a WarriorZ bottle-packer inquiry.
Official sources
Sources and verification basis
These references support the documented facts, calculations, or engineering boundaries used in this article.